
Overview
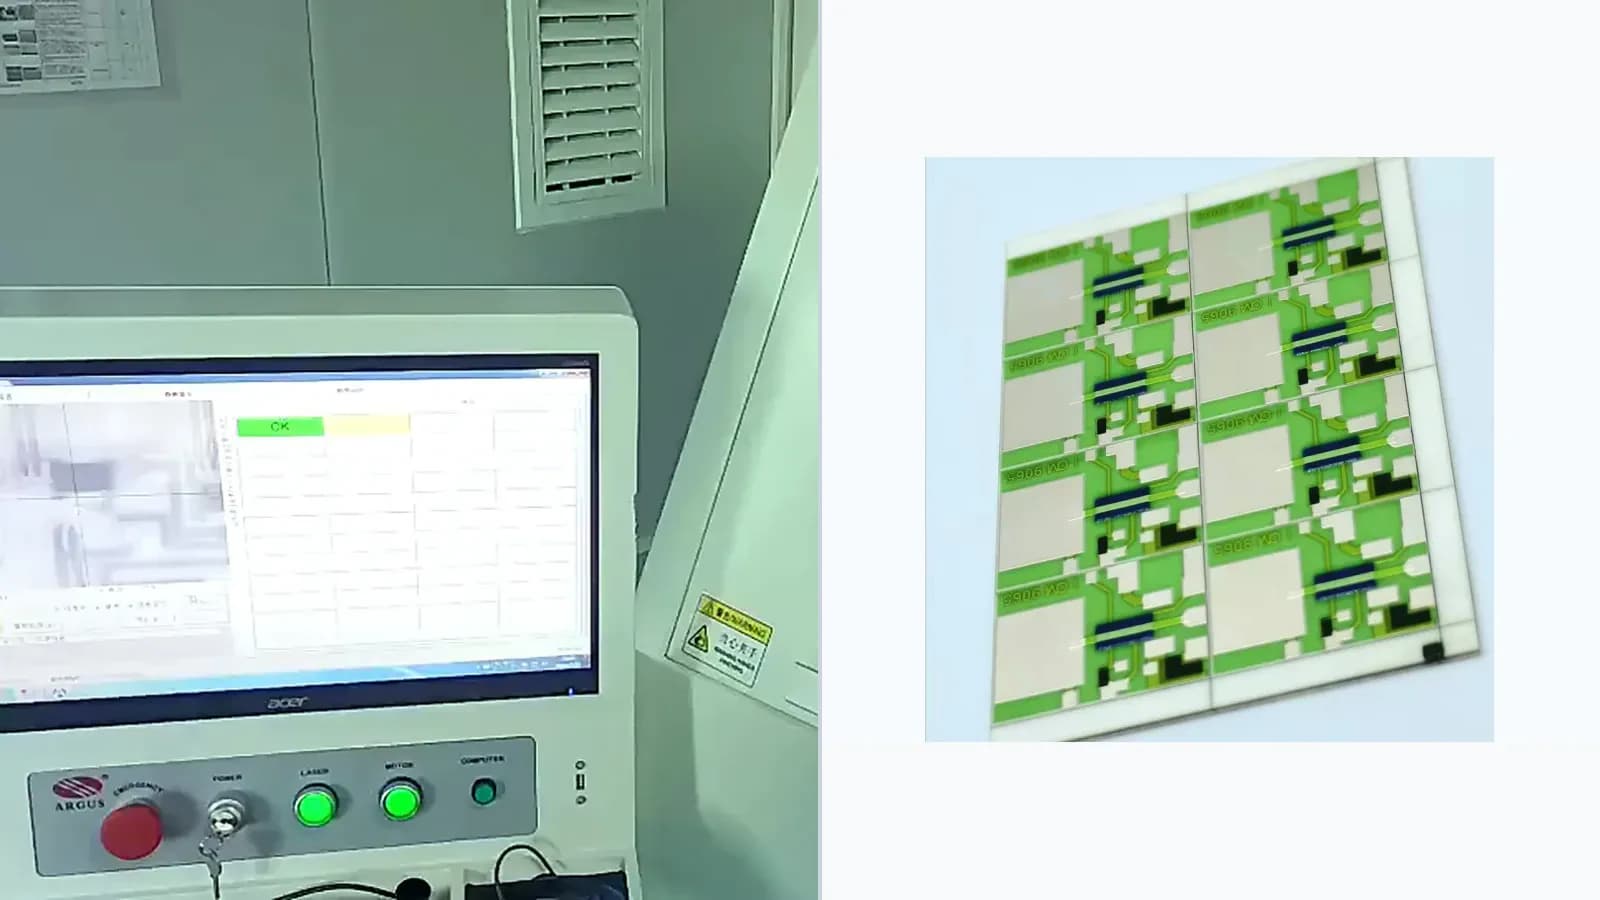
This process control record treats Laser Trimming Process Control as a controlled release sequence rather than a machine-list claim. It connects incoming inputs, process variables, inspection points, exceptions, and traceability to the failure each control prevents.
Control sequence
The order makes assumptions and ownership visible before a result is promoted to a requirement.
- 01
Release the input revision
For Laser Trimming Process Control, close remaining assumptions and link the quoted or released scope to the drawing revision, evidence set, owner, and change-control plan.
- 02
Confirm materials and tooling
For Laser Trimming Process Control, document the functional requirement, operating boundary, interfaces, quantities, and acceptance owner against the current drawing.
- 03
Control the process window
For Laser Trimming Process Control, complete control the process window against the controlled drawing, named assumptions, responsible owner, required evidence, and release decision.
- 04
Measure the critical output
For Laser Trimming Process Control, agree the inspection method, sample plan, acceptance criteria, traceability, and report format before validation.
- 05
Record exceptions and disposition
For Laser Trimming Process Control, complete record exceptions and disposition against the controlled drawing, named assumptions, responsible owner, required evidence, and release decision.
Engineering review matrix
Each row links a design variable to evidence that can support a drawing or release decision.
| Variable | Control question | Verification route |
|---|---|---|
| Functional objective | For Laser Trimming Process Control, value adjustment, hole creation, separation, or marking use different beam, geometry, and acceptance logic. | Release the operation only against a named drawing feature or measured target. |
| Energy interaction | Wavelength, pulse, energy, focus, speed, repetition, assist, and material absorption control removal and thermal damage. | Establish a process window on representative stacks and monitor critical parameters. |
| Geometry | Kerf, taper, recast, debris, radius, path, trim shape, and distance to conductors or edges influence function. | Inspect the processed feature using its drawing datum and suitable method. |
| Measurement loop | For trimming, probe condition, settling, increments, algorithm, overshoot margin, and final verification form a closed loop. | Record initial, target, final, and stability values with program and lot identity. |
| Post-process integrity | Cleaning, microcracks, heat-affected regions, insulation, strength, and assembly must remain acceptable. | Use visual, dimensional, electrical, and reliability checks selected for actual risk. |
Failure controls
These are review prompts, not evidence that every risk applies or that every test is available.
- A
Overcut, overshoot, taper, or geometry outside tolerance
- B
Recast, debris, carbonization, microcracking, or heat-affected damage
- C
Electrical instability from trim geometry or inadequate post-trim margin
- D
Registration loss between program, datum, artwork, and revision
Inputs for a practical review
Unknown values may be labelled unknown. The review should convert uncertainty into an explicit decision or validation task.
Send Drawings- 01
Feature or electrical target and drawing datum
- 02
Material stack and laser-access constraints
- 03
Geometry, edge quality, damage, and cleanliness acceptance
- 04
Measurement and program control for closed-loop trimming
- 05
Post-process electrical, mechanical, and reliability checks