
On this page
Prepared by Chipsimple Engineering Team, Engineering and technical content review
Published online August 8, 2026 · Reviewed August 8, 2026
Scope: This is an RFQ and control-plan framework, not a promise that every listed process or test applies to every product. The drawing, contract review, risk assessment, and applicable customer or regulatory requirements determine the released plan.
Many quotation problems begin before a supplier calculates price. A buyer sends an outline drawing, photograph, or nominal resistance, while critical information remains in email or in the final assembly team’s experience. The supplier fills gaps with assumptions, and those assumptions reappear as tooling changes, prototype delays, or disputed results. A stronger workflow converts the commercial request into controlled technical inputs before production release.
Separate confirmed requirements from open targets
The RFQ should distinguish mandatory acceptance criteria from values that may be optimized during development. A fixed outline, connector interface, safety limit, or resistance curve may be mandatory. A proposed substrate grade, track layout, paste family, or packaging method may remain open. Marking the difference allows a practical suggestion without silently changing the requirement.
Each project needs one controlled source for dimensions and revisions. The package can include PDF, DXF, Gerber, STEP, or another format, but conflicts require stated precedence. Units, datums, tolerance conventions, surface and edge requirements, and critical characteristics should be explicit. Samples are useful references, yet a sample is not a complete specification because its production history, material grade, and acceptable variation may be unknown.
Define the functional stack and downstream assembly
List substrate, conductors, resistors, dielectric or crossover layers, protective coatings, terminal finishes, and backside or edge features. If exact material is not fixed, state the properties or compatibility an alternative must meet. Downstream assembly information is essential: solder alloy and profile, wire bond, die attach, adhesive, cleaning chemistry, coating, connector load, fasteners, and thermal interface can change the correct metallization and validation route.
Electrical requirements should include more than nominal resistance. Define measurement points, reference temperature, tolerance, TCR where relevant, voltage, current, power, duty, insulation, and position curve or heater zone. For RF structures, provide impedance target, frequency range, reference plane, stack assumptions, and test method. For sensors, provide mechanical datums and readout circuit. For heaters, provide thermal boundary conditions.
Convert application risk into an inspection plan
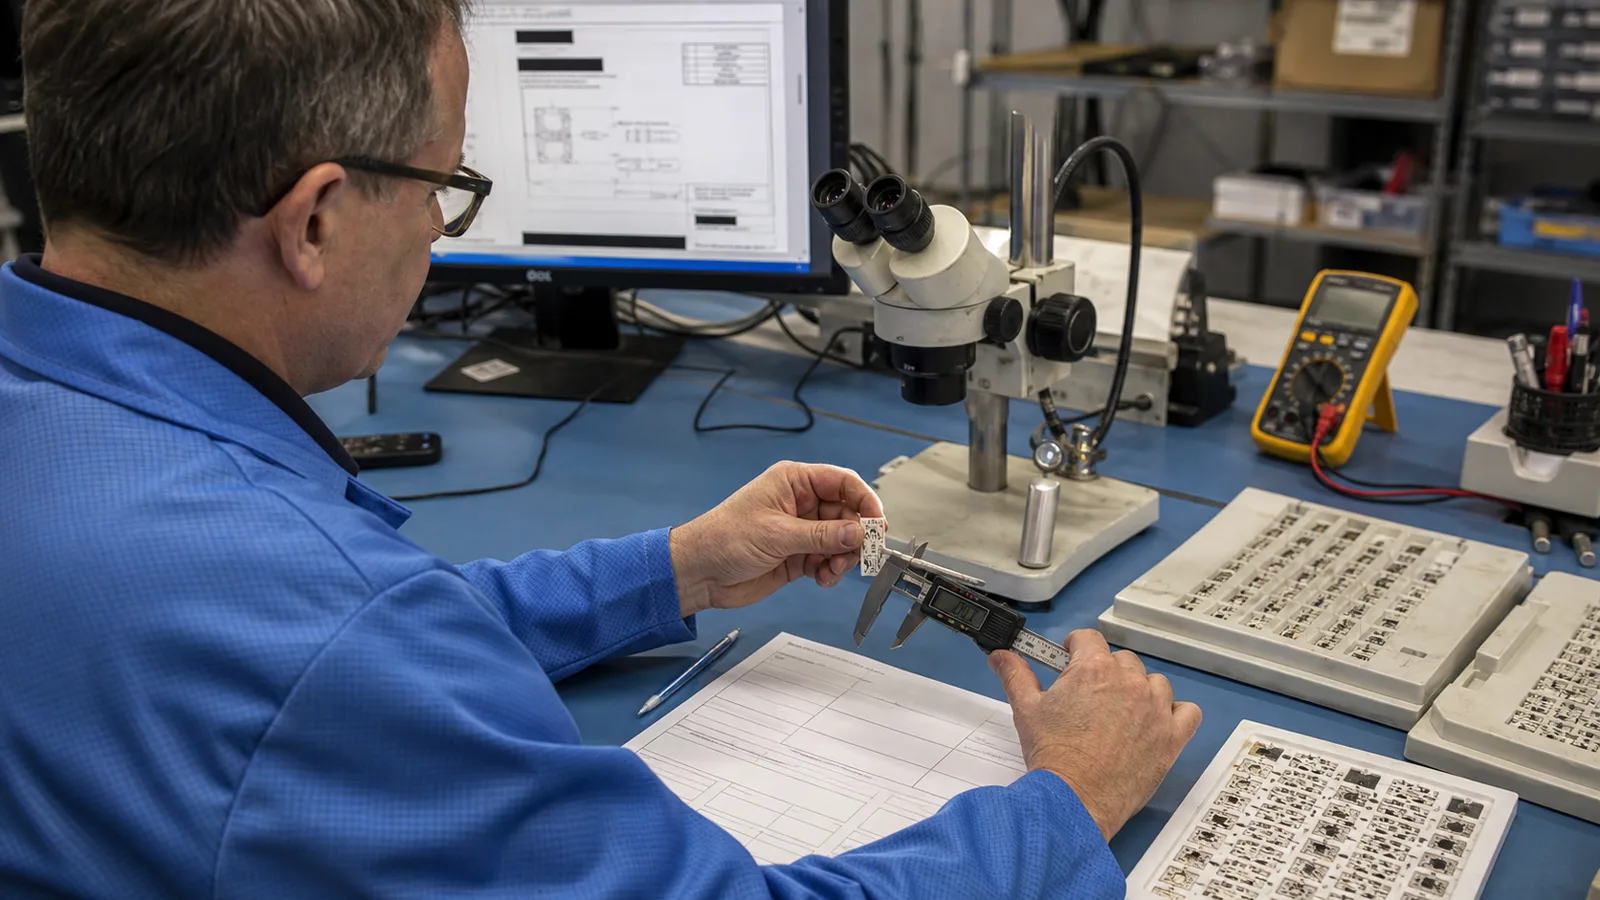
A control plan identifies each critical characteristic, stage, method, equipment or fixture, frequency, acceptance limit, record, and reaction to failure. Not every feature requires the same control. Focus tighter controls on characteristics affecting fit, safety, electrical function, thermal performance, assembly yield, or field reliability.
Incoming checks can include substrate identity, dimensions, flatness, surface, edge quality, and approved lot documents. In-process checks can cover registration, material identification, drying and firing records, as-fired resistance, trim result, dielectric coverage, and visual defects. Final checks can include dimensions, continuity, resistance or curve, insulation, terminal condition, solderability or bondability when specified, marking, cleanliness, and packaging.
IEC 60115-1 establishes generic terminology, inspection procedures, and test methods for fixed resistors. IEC 60068-1 describes a framework for selecting environmental methods and severities appropriate to transport, storage, and use. These references create common language, but do not replace the customer detail specification or choose a pass limit for a custom circuit.
Prototype evidence must identify the tested configuration
A report is useful only when it identifies what was tested. Record drawing revision, material system, lot or sample identity, fixture, instrument, calibration status, conditions, results, deviations, and approval. Photographs should show relevant features and scale where useful; they are not sole evidence for an electrical or dimensional result.
Before batch production, close deviations and update the drawing, work instructions, tooling, inspection program, and acceptance plan. A golden sample can support visual comparison, but it should be accompanied by controlled documents because samples age, can be damaged, and cannot communicate hidden material or test requirements.
Repeat production needs change control and traceability
Traceability is proportionate to risk and contract requirements. Useful records can connect the shipped lot to substrate and functional-material lots, key process routes, inspection results, nonconformance disposition, and release authorization. Retention period and report format should be agreed. Avoid documents that do not support a decision, but do not omit records needed to investigate a future issue.
ISO 10013 gives guidance for documented information supporting an effective quality management system and tailored to organizational needs. That principle matters in custom manufacturing: documents should control work and preserve evidence, not exist only as a large template package.
Minimum RFQ and release checklist
- Controlled drawing set, precedence, revision, units, datums, tolerances, and critical characteristics.
- Function, substrate and layer stack, material constraints, finishes, and required substance documentation.
- Electrical, thermal, mechanical, environmental, and life requirements with test conditions.
- Assembly, cleaning, coating, mounting, sensing, and connector interfaces.
- Prototype quantity, forecast, packaging constraints, schedule, and approved alternatives.
- Inspection items, sampling or full checks, report format, traceability, qualification, and retention.
- Change-notification rules for material, process, tooling, location, or critical supplier.
A practical quotation may still contain open points. The discipline is to list them, assign responsibility, and close them before release. That protects the buyer from receiving a part that only resembles the drawing and the manufacturer from being judged against requirements it never received.
Primary references
Turn the RFQ into a controlled review
Send the drawing, function, material and layer requirements, assembly conditions, environment, quantity, and required inspection evidence.