
On this page
A lid that clears the highest wire loop on a static drawing can touch it during closure, handling or pressure loading. The relevant dimension is the smallest separation between the completed wire envelope and the inward-moving lid surface. Review that separation after including actual support conditions and assembly tolerances. A nominal cavity height does not establish an operating clearance, and a clear bonding-tool approach does not establish clearance after the tool has left.
System boundary
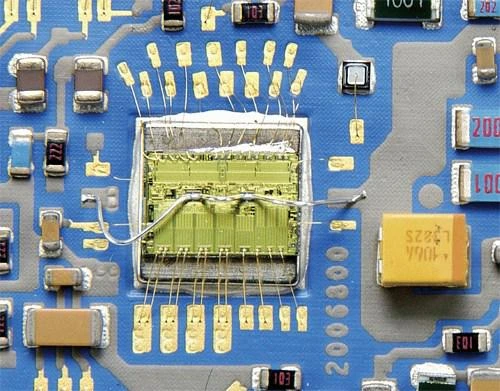
A ceramic hybrid with completed wire bonds and a separately installed lid. The review addresses lid-to-wire interference; it does not assign wire-bond strength, package hermeticity or an electrical safety spacing.
Integration interfaces
| Interface | Required input | Thick film role | Validation owner |
|---|---|---|---|
| Wire loop to lid underside | Maximum measured loop envelope and minimum local lid position. | Locate the bond pads and wire endpoints relative to the ceramic datum. | Wire-bond and package designers reconcile the clearance model. |
| Lid rim to housing seat | Seat geometry, attachment thickness, tilt and closing sequence. | Maintain the specified ceramic location inside the assembled package. | Mechanical integrator defines the complete stack. |
| External load to lid | Pressure difference, handling contacts and support stiffness. | Remain outside the moving enclosure envelope. | System mechanical owner validates representative loaded states. |
Integration risks
| Risk | Control or verification | Validation owner |
|---|---|---|
| A locally deflected lid contacts a loop despite adequate nominal height. | Evaluate local clearance throughout the specified loading sequence. | Package mechanical owner. |
| Adhesive or a seal feature enters from the side. | Include the inward material envelope independently of cavity height. | Assembly process owner. |
| Inspection misses temporary contact during closure. | Observe the closing path and retain loop shape before and after it. | Assembly and test owners. |
System integration decisions
- Use a common height datum for the wire envelope, lid underside and package support.
- Check the spatial deflection near each loop, not only the lid's largest displacement elsewhere.
- Keep mechanical noncontact, electrical spacing and package sealing as separate acceptance questions.
Put the cavity and the loops on the same datum
Choose a physical reference that survives assembly, such as a defined package seating plane. Express the ceramic top surface, die attachment, wire-loop envelope and lid underside relative to that plane. Combining a loop height measured from the die with a cavity dimension measured from the ceramic can omit the die and attachment thickness entirely.
Record the actual high points and lateral positions of the loops. A single maximum height is conservative only when the lid's minimum underside height applies across the same region. Nearby components, ribs or a sloping lid may produce a smaller local gap away from the tallest loop. Use the assembled spatial relationship instead of pairing unrelated global maxima and minima.
Include the lid installation path
Follow the lid from first engagement to its final seat. A hinged approach, tilted placement or locating feature can sweep a corner below its final position. The first point of contact with a gasket or adhesive bead may temporarily define a pivot. A finished assembly photograph cannot demonstrate that the wire avoided this earlier envelope.
Check the proposed closing fixture and any tool pressing on the lid. A loading pad applied near the center creates a different deflection pattern from force applied around the rim. Keep tools and temporary locating features in the same interference review. The method should not depend on pushing against the lid until resistance is felt; that resistance could be a wire or component rather than the intended seat.
Calculate a local worst-position gap
For an illustrative location, assume a nominal lid underside 1.40 mm above the chosen ceramic datum and a maximum loop envelope of 0.85 mm. Allow 0.12 mm for downward lid position tolerance, 0.08 mm for relative stack movement and 0.18 mm for the specified local inward deflection. The remaining mechanical gap is 1.40 − 0.85 − 0.12 − 0.08 − 0.18 = 0.17 mm.
These assumed dimensions show how a generous-looking 0.55 mm nominal separation can shrink. The result is not a recommended clearance or proof of acceptability. Determine whether each term is already represented in a measured assembled envelope before subtracting it again. Correlated movement of the ceramic and housing must be expressed as relative movement, not two independent penalties.
g_min(x,y) = h_lid,nom(x,y) − h_wire,max(x,y) − e_lid − e_stack − w_in(x,y)
- g_min: screened remaining local mechanical gap, in mm.
- h_lid,nom: nominal underside height at the evaluated position, in mm.
- h_wire,max: maximum completed-wire envelope at that position, in mm.
- e_lid and e_stack: nonduplicated downward relative-position allowances, in mm.
- w_in: inward lid deflection under the stated load at coordinates x and y, in mm; x and y are planar coordinates in mm.
Conservative subtraction for a stated local position and load state. The model does not predict deflection; it requires measured or appropriately analyzed deflection and separately reviewed electrical spacing.
Apply loads that can actually reach the lid
List the pressure difference across the enclosure, installation loads, foreseeable service handling and any contact with an adjacent assembly. A sealed cavity can experience a pressure difference when temperature or external pressure changes, but the pressure history must come from the system definition. Do not treat room-pressure assembly as zero differential pressure for every later condition.
Use the real support at the rim when measuring or analyzing deflection. A lid supported continuously behaves differently from one held at several tabs. Attachment compliance, seal compression and housing motion may all contribute. A material stiffness value alone cannot establish the loaded shape; dimensions, restraints and force distribution are needed. Compare local predicted movement with an appropriate physical measurement before relying on a small residual gap.
Reserve clearance for material entering from the side
Adhesive squeeze-out, seal protrusion and displaced gasket material may enter the cavity near the wire endpoints. Their envelope is not captured by a central lid-height check. Show the permissible inward extent at the attachment region and inspect the state after seating, when the material has moved from its initial dispense shape.
For a concrete decision, suppose a loop clears the underside throughout the load cycle but its descending end passes through the possible adhesive fillet. Increasing center cavity height does not fix that interference. The relevant change is the fillet envelope, wire route or attachment boundary, followed by review of the affected assembly process. Do not alter a qualified adhesive quantity or cure recipe informally to recover drawing space.
Use observations to locate the interfering feature
Retain loop images before closure and after a controlled evaluation of the representative package. Match each wire by pad coordinates rather than by a general photograph of the cavity. An unchanged final electrical reading cannot exclude a temporary mechanical touch, while a changed reading alone does not identify a lid collision.
Choose observation methods that do not add foreign material to the wire or modify the available gap. Witness materials, transparent development lids or instrumented fixtures require their own equivalence assessment. A stiff transparent lid, for example, may preserve visibility while eliminating the deflection being investigated.
| Observation | Focused check | Likely design variable |
|---|---|---|
| Loop changes only during tilted closure | Observe the approach before final seating | Closing path and locating sequence |
| Central loops move under pressure difference | Compare local lid displacement with loop positions | Lid span, support and pressure boundary |
| Peripheral wire enters attachment material | Map inward fillet after seating | Attachment envelope and wire route |
| Gap changes with one housing screw | Track housing and ceramic relative motion | Stack support and assembly sequence |
| Electrical change without visible contact | Investigate bond and conductor paths independently | Do not assume the lid is the cause |
Do not equate noncontact with sufficient electrical spacing
A positive mechanical gap only says the simplified envelopes do not intersect. A conductive lid near a wire can create electrical coupling or require a defined insulation distance. Those questions depend on wire potential, lid connection, waveform, environment and end-product requirements. Keep them visible instead of reporting the mechanical calculation as an isolation rating.
Likewise, a lid modification that improves clearance may change sealing, heat transfer or electromagnetic behavior. Review those interfaces with their owners. The completed wire geometry remains tied to the selected bonding process; lowering a loop is not a purely mechanical edit if it changes heel shape, bonding sequence or qualified wire behavior.
Release the loaded envelope with the assembly drawing
Provide the reference plane, local loop envelopes, lid surface map, tolerance terms and evaluated load cases. State how deflection was obtained and which physical configuration was measured. Include the closing sequence and the attachment-material boundary, with images captured before hidden surfaces become inaccessible.
Reopen the interference check when lid thickness, rim support, seal, fixture, pressure history, die height or wire programme changes. The useful deliverable is a location-specific remaining gap through the actual assembly and service states, accompanied by the applicable mechanical and electrical acceptance decisions. It is not a universal minimum cavity height for every wire-bonded module.
Send the lid and completed-wire envelopes
Provide the assembled coordinate system and loading states so local lid movement can be compared with the actual wire loops.
- Package, ceramic, die and lid drawings with common height datums and tolerances.
- Completed-loop measurements and pad locations, including peripheral descending wires.
- Rim support, closing fixture, attachment-material envelope and pressure or handling loads.
- Local deflection observations, preclosure images and separate electrical-spacing requirements.
The drawing-upload form loads as you reach this section.